Food & Beverage · Case Study
How a Barrier Pouch Added 45 Days of Shelf Life at Three Cents More
Rare Breed Coffee, a mid-sized food brand, was selling into national retail on a generic 3-mil pouch. The barrier was adequate, the story was not, and the pouch was quietly costing roughly $12,000 a month in stale stock.
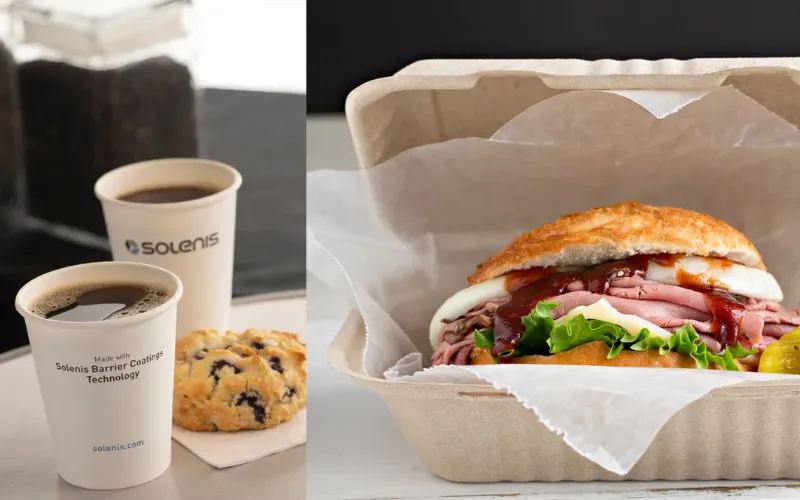
The rebuilt pouch: FSC kraft face, EVOH barrier behind 
Extraction testing before the material roll was signed off 
The launched pouch, six months later
The Result, Up Front
- +18%
- Repeat purchasesover six months
- +45
- Days of shelf lifewith no moisture penalty
- −15%
- Freight costdimensional weight
- +$0.04
- Net margin per unitafter a three-cent rise
- Client
- Rare Breed Coffee
- Industry
- Food & Beverage
- Brief
- Kraft-EVOH barrier pouch
- Order
- Retail-ready, shelf display included
- Timeline
- Six months to the result
01 · The Challenge
A Pouch That Protected the Product and Nothing Else
The brand was on a generic 3-mil PET/PE pouch. It kept the product fresh and did nothing else: no story on the shelf, no reason for a shopper to come back, no argument for a retailer to keep the facing.
The obvious replacement — a compostable film — failed on the machine before it reached a shelf.
Compostable film warped under the heat sealers
On the machine trial the new film warped under standard heat sealing. The high heat opened micro-leaks along the gusset, which meant constant daily rework instead of a cleaner pack.
Twenty percent more cost, with a weaker barrier
Greener alternatives were quoted about 20% higher per unit, and without validated barrier data behind them. Oxygen and moisture transmission have to be measured on the product, not inferred from a material name.
Twelve thousand a month in stock nobody could sell
The old pouch was costing roughly $12,000 every month in stale, wasted inventory, while national retailers signalled a Q4 delisting over new recycled-content expectations.
A seal that snapped at twelve Newtons
On a calibrated tensile machine the legacy bottom seals failed at 12 Newtons of force. That is a pouch that survives the warehouse and not the journey.
Without OTR and MVTR validation, this eco-film just creates stale food.
02 · What We Changed
A Structure, Not a Material Swap
Forty hours of floor trials across fifteen candidate laminates produced one answer: keep a kraft face for the shelf, and put the barrier where a barrier belongs.
An FSC kraft face at 150 GSM
The outer layer is FSC-certified kraft at 150 GSM. It is the part a customer touches, and it carries a paper story that a plastic film cannot.
A high-barrier EVOH layer behind it
Behind the kraft sits an EVOH barrier film. A fully compostable structure was evaluated and rejected: those materials do not yet carry the grease resistance this product needs.
A reseal that survives twenty openings
A press-to-close PE zipper was specified to hold past twenty uses, because freshness after the first open is what earns the second purchase.
A seal temperature the material actually wants
Sealing temperature went from 145°C to 165°C, with jaw pressure up 12%. Roller cleaning went into the startup checklist every two hours, which took startup scrap to zero.
The Gated Sequence
Five Gates, Each With a Release Condition
Gate 1
Trial on the real line
Released after a 500-unit run on the actual filling machine. A lab specification rarely accounts for your machine tension or your daily heat fluctuation.
Line trials
Gate 2
Validate the barrier
Released on transmission data measured at 23°C and 50% relative humidity, taken off a permeation analyzer rather than a datasheet.
Laboratory
Gate 3
Prove the seal under pressure
Released on burst testing. The legacy pouch failed at 18 PSI and the new structure held to 32.
Quality control
Gate 4
Clear it for food contact
Released on a hexane extraction test against FDA extraction limits, run on the inner film layer before the material roll was signed off.
Compliance
Gate 5
Take the cube out
Released when the pack came in 12mm narrower and still held the same volume — 24 more pouches in every master carton.
Logistics
A barrier film is a lab result until it meets a heat sealer. The number that decided this pack was not the oxygen rate — it was the twenty degrees the seal head had to move.
03 · What the Numbers Say
The Number, and How to Verify It
The headline claim is 45 extra days of shelf life from a pouch that costs three cents more. The table below is the whole of it.
| What moved | Before | After | How it was measured |
|---|---|---|---|
| Oxygen transmission | 2.5 cc/m²/day | 0.8 cc/m²/day | Permeation analyzer at 23°C, 50% relative humidity |
| Moisture transmission | 1.2 g/m²/day | 1.3 g/m²/day | Same instrument, same conditions — held, not improved |
| Burst strength | 18 PSI | 32 PSI | Air probe, pressurised until the seal fails |
| Food waste | 14% of production | 2% | Counted from the spoilage records kept on the line |
| Unit cost | $0.15 | $0.18 | Verified at the production tier, not estimated |
Transmission rates were measured on the same instrument at 23°C and 50% relative humidity, before and after. Burst figures come off the pressure rig, and the shelf-life extension was modelled from accelerated aging and then checked against the client’s own quarterly sales data.
We initially fought the higher unit cost. But the new material stabilized our fill line instantly. We stopped throwing away stale inventory, and our retail partners love the premium look.
04 · What to Demand Next Time
Four Questions Worth Asking Before You Swap a Pouch
A material swap is the cheapest-looking change in packaging and the easiest one to lose money on. These four questions are the difference.
Ask for the barrier number, not the material name
A number on a supplier datasheet describes a film, not your product. Ask for the measurement taken on what you actually pack, with its test conditions attached.
Trial on your line, at your temperature
Heat-sealing behaviour changes with the machine and with the room. A 500-unit run on the real line costs a shift and prevents a launch.
Price the waste next to the pouch
The pouch went up three cents. Stale inventory went from 14% to 2%, which is roughly five cents a unit back. Model both lines, or the cheaper pouch wins an argument it should lose.
Measure the carton, not the pouch
Dimensional weight is charged on the box, not the product. Twelve millimetres off the pack width put 24 more pouches into every master carton.
Shelf life and food waste are the same number. Forty-five more days on a pouch is not a packaging win, it is a reduction in what the retailer throws away.
Have a Pouch That Goes Stale on the Shelf
Send us the film and the failure it is causing. The reply names the barrier you actually need, and what the current structure is costing in waste.
Start a Project