Beauty & Skincare · Case Study
How We Took a Skincare Launch from a 15% Leak Risk to 0% Across 50,000 Units
Wildsmith Skin, preparing a first at-scale run for Western retail and DTC. The order was 50,000 glass-dropper units, and the closure thread failed a torque check before mass production had started. The brand halted the trial run rather than ship it.
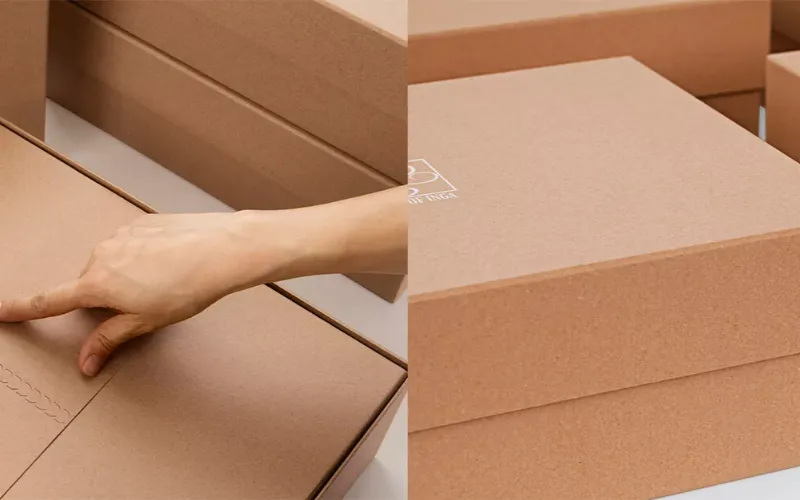
The launched system: PETG jar and rigid box 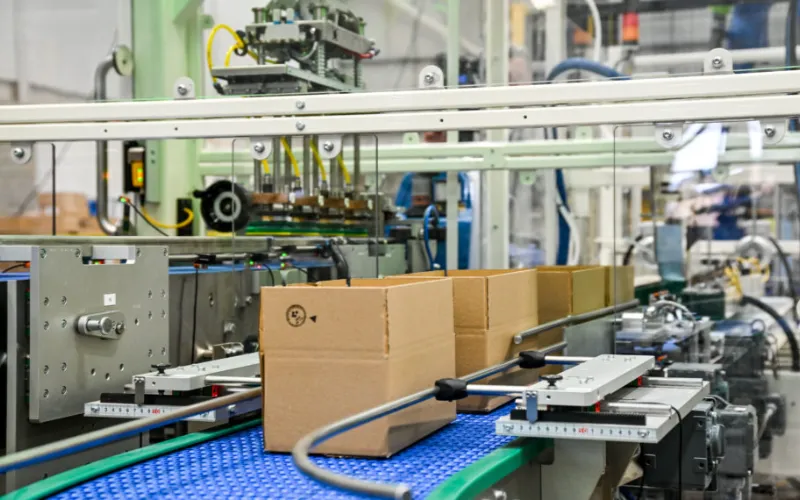
Primary and secondary, rebuilt as one structure 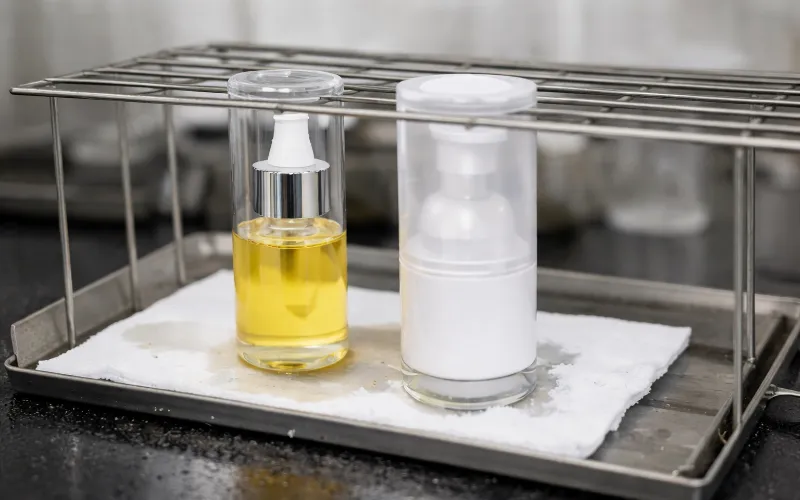
Vacuum held at −0.06 MPa, three minutes
The Result, Up Front
- 0%
- Transit leakageacross 50,000 shipped units
- 22%
- DTC sales upliftlaunch window
- 40 hrs
- QA approvals savedper batch
- 12%
- Lighter shipmentwall structure
- Client
- Wildsmith Skin
- Industry
- Beauty & Skincare
- Brief
- PETG jar + rigid box system
- Volume
- 50,000 units, first run
- Timeline
- One quarter to launch
01 · The Challenge
The Flaw a Sample on a Table Cannot Show
The brand approved the jar from a handmade prototype. It sat on a boardroom table, it looked immaculate, and it passed the only checks that room could offer.
The fault only existed at production speed. Run unchanged, the projected rate in air freight was 15% — a figure nobody had a reason to doubt until the pilot run.
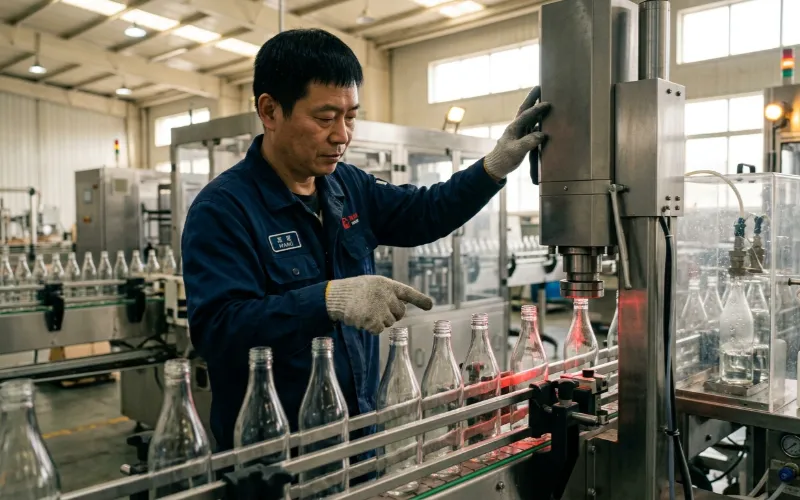
The thread only fails in motion
A prototype is capped by hand. The fault appears under the capping machine, where uneven grip becomes a gap — which is why the sample inspection passed and the trial run did not.
Ten closures is all it takes
Standard acrylic micro-fractured at the neck thread after ten tight closures. On a desk the jar reads as flawless; under air-freight pressure the wall is what fails first.
A visual check cannot see a micro-gap
A container can pass a visual inspection and still leak. Pressure drops during flight force liquid through openings too small for an inspector to find by eye. Only a vacuum hold catches them.
What shipping it unchanged would have cost
Four costs landed on the brand at once, and only one of them was the product:
- Refund claims on every unit that arrived wet
- A launch window pushed back by reworking bad batches
- Retail and DTC trust, which a leak destroys faster than a price rise
- A higher landed cost per unit once rejects were counted
The glass thread tolerances vary by a fraction of a millimeter. If we run this at full production speed, the closure grips unevenly. It will leak during air freight.
02 · What We Changed
Three Layers, Fixed in Order
A cosmetic tweak would not have survived global logistics. The fix ran in three layers — the primary container, the presentation system, and a control cadence that put a measured number on every batch.
Why the thread was the whole problem
Acrylic, as supplied
The neck thread cracks under repeated closures. The cap torques down unevenly, and the pressure hold never gets started.
PETG, as rebuilt
The same profile in a material that keeps its shape under load. Sampled units sealed on the first hold, with no bubble trail in the chamber.
Move the primary container off acrylic
Acrylic looks right on a desk and gives way under air freight. All key components moved to PETG: clearer, far higher impact resistance, and a thread that survives a full production run.
The wall was rebuilt as a lighter, more durable profile, which took 12% off shipping weight without changing the silhouette.
Rebuild the presentation box as a structure
The old box had no rigidity and quietly undercut the price point. The replacement used FSC-certified board at 1,200 gsm, with a liner cut to the bottle layout so nothing shifted in transit, finished in a soft-touch matte.
Put a Number on Each Batch
Incoming board and components gauged before they reached the line. A pilot assembly review tested the closure against the capping machine’s real torque limits. An AQL 2.5 sampling plan was locked for each production lot before the first one ran.
Prove the seal, not the look
Metallic pump components ran 96 hours of salt spray to ASTM B117, so gold finishes hold in a humid bathroom. Finished jars then held vacuum at −0.06 MPa for exactly three minutes across fifty randomly sampled units — the test that catches a gap a visual check passes.
The Gated Sequence
Five Gates, Each With a Release Condition
Gate 1
Diagnose on the line
Released only once the fault reproduced under machine torque, not in a single hand-capped sample.
QC inspector
Gate 2
Re-spec the structure
Released when the redrawn wall hit its weight target without losing the rigid feel the price point depends on.
Gate 3
Rebuild the secondary
Released when the liner sat the bottles with no movement under shake, and the printed sheet held the colour target.
Interior fitment
Gate 4
Verify under load
Released on instrument readings alone — every figure signed off had come off a gauge, never an opinion.
Leak and pressure testing
Gate 5
Ship and re-measure
Released to the brand only after the arrival data matched the factory data, unit for unit.
Operations manager
Two claims sit on a pack like this one: an FSC board and a polymer chosen for impact. The first is a chain of custody; the second is only as good as the pressure data behind it.
03 · What the Numbers Say
The Number, and How to Verify It
The headline claim is 0% leakage across 50,000 units. The table below is the whole of it — what moved, and the instrument behind each figure.
| What moved | Before | After | How it was measured |
|---|---|---|---|
| Transit leakage | 15% projected | 0% measured | Fulfillment logs; closure torque re-measured on arrival |
| Neck thread | Micro-fracture at 10 closures | Intact across the run | Digital calipers on thread pitch and closure fit |
| Metallic pump finish | Not tested | No oxidation | 96-hour salt spray, ASTM B117 |
| Shipment inspection | Visual check | AQL 2.5 sampling | Pre-shipment sampling plan, every lot |
| Shipping weight | Baseline | −12% | Lighter wall structure, same silhouette |
The operations team tracked exactly 50,000 units from the Shenzhen assembly floor to the Western distribution center, and closure torque was re-measured with a digital meter on arrival. The finished system passed ISTA 3A transit testing, and the raw fulfillment logs were audited against the claim before this page was written.
Customers immediately praised the premium weight and feel of the rigid box. We saw a complete drop in damage claims. The new architecture did not just fix our leak problem — it elevated the perceived value and supported a higher retail price point.
04 · What to Demand Next Time
Four Questions Worth Asking Before You Scale
None of this is specific to skincare. Any buyer approving a container in China can ask the same four things, and each one is cheap to ask before tooling and expensive to ask after.
Approve the mechanics, not the prototype
A sample signed off in a meeting room has never been through a capping machine. Name the torque figure the closure must reach, and ask for it demonstrated before tooling is paid for.
Set the pass/fail before the first lot
Name the AQL level, the sampling plan and the measuring instrument in the supplier agreement. Vague quality language is what lets a defect reach a customer with every inspection signed off.
Treat a material upgrade as a margin decision
PETG cost more per unit. It also ended the replacement shipments, and a 12% drop in replacement waste paid the difference back. Price the failure, not just the piece.
Read raw defect data, not a summary
Ask for the inspection records rather than a certificate. The figure that matters is the one on the caliper, and it should come from your supplier’s own paperwork.
A rigid box is not packaging around a product; it is the first physical evidence of what the product costs. Which is why a box that flexes in the hand undoes the price on the label.
Have a Leak, a Claim Rate, or a Crushed Corner
Send us the failure you are trying to move. The reply names what to change first, and what leaving it alone would have cost.
Start a Project